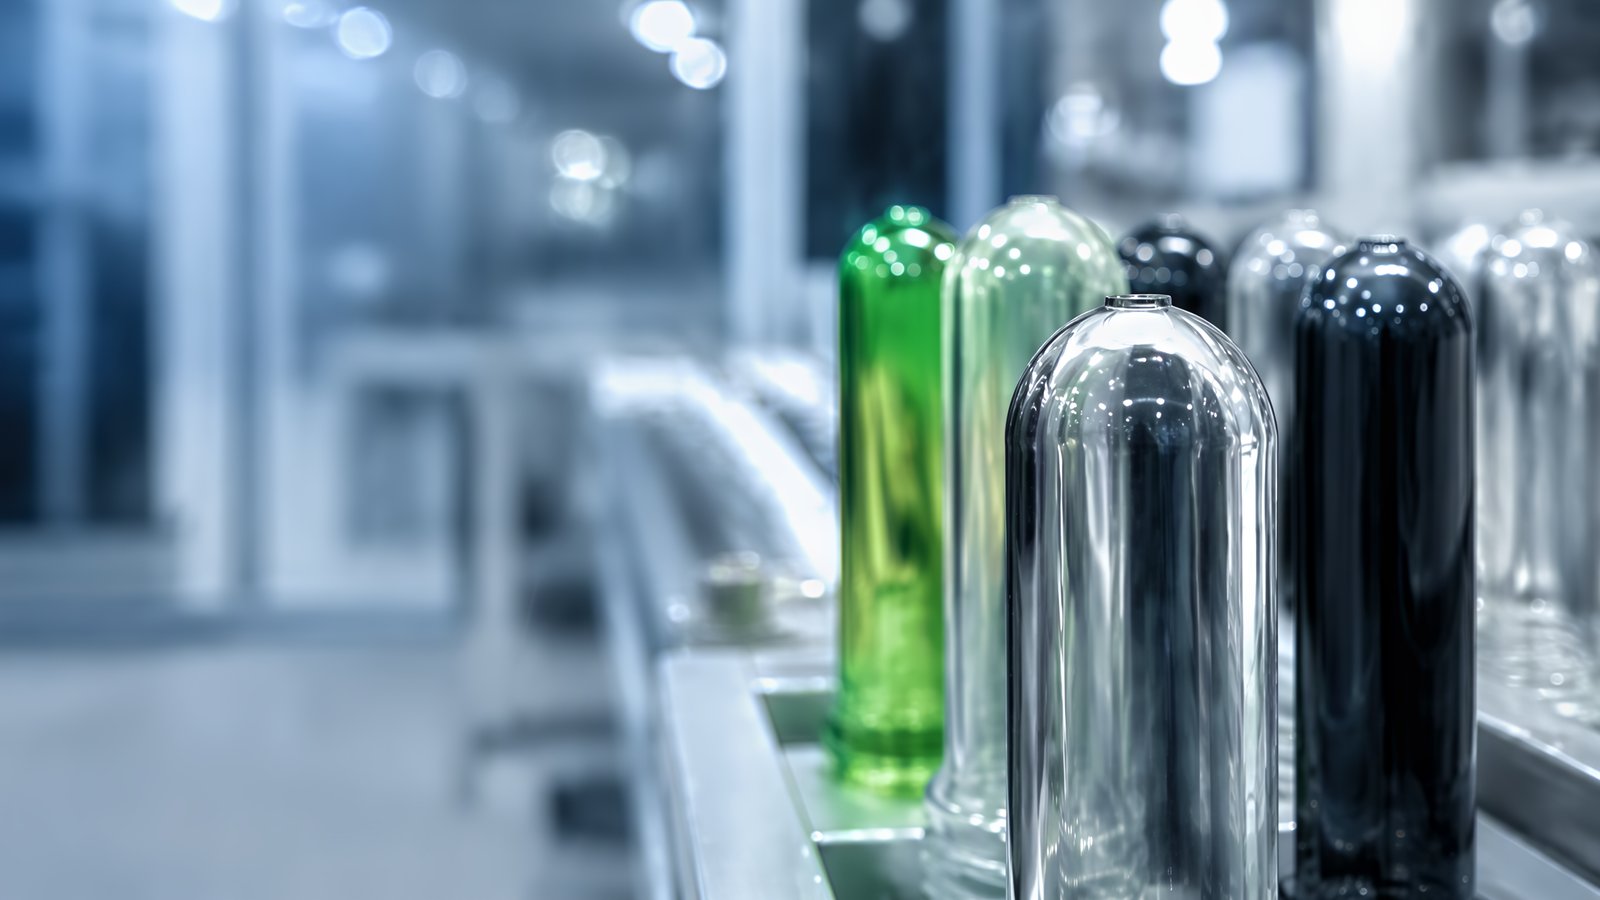
When selecting injection molding equipment for PET packaging, one engineering decision affects cycle time, material yield, and long-term operating cost: choosing between a hot runner vs cold runner preform mold system. Both configurations deliver the same end product—a PET preform ready for blow molding—but they differ fundamentally in how molten plastic travels from the machine nozzle to the cavities. Understanding these differences helps production managers match mold technology to volume targets, budget constraints, and quality requirements.
What Is a Hot Runner System in PET Preform Molds?
A hot runner system keeps the melt channel at processing temperature throughout the entire injection cycle. Instead of allowing plastic to cool in runners and sprues, heated manifolds and nozzles maintain the PET in a molten state. When the mold opens, only the finished preforms are ejected; there is no solidified runner network to remove and recycle.
Components of a Heated-Runner System
The key assemblies include:
- Manifold plate – distributes melt from the single machine nozzle into individual drops
- Heated nozzles – direct molten PET into each cavity gate
- Temperature controllers – typically one PID zone per nozzle tip to maintain ±1–2°C stability
- Gate inserts – thermal or valve-gate designs that control drool and vestige
Temperature Control and Maintenance
Because PET is sensitive to thermal degradation, hot runner systems require precise temperature control. Each zone runs between 260°C and 280°C, depending on resin IV and preform weight. Maintenance involves periodic inspection of heater bands, thermocouple calibration, and cleaning of nozzle tips. Downtime for a heated manifold is usually scheduled rather than frequent, but when it occurs, it requires trained technicians.
What Is a Cold Runner System for PET Preforms?
A cold runner system is the traditional layout where molten PET flows through unheated runners and a central sprue. As the mold cools, the plastic in these channels solidifies along with the preforms. After ejection, operators or an automated device separates the runners from the parts, and the solidified scrap is ground and reintroduced into the process.
Components of a Traditional-Runner System
- Sprue bushing – receives melt from the machine nozzle
- Runner channels – trapezoidal or round passages machined directly into the A/B plates
- Sub-runners and gates – split flow to each cavity
- Ejector system – pushes both preforms and the runner block out of the mold
Sprue and Runner Waste
In a cold runner setup, the weight of the solidified runner network typically equals 15–25% of the total shot weight, depending on cavity count and runner layout. This material is not lost—it is reground and reused—but the regrind ratio in PET must be managed carefully to avoid IV drop and color variation. For light-colored or transparent preforms, excessive regrind can create haze or yellowing, so many processors sell runner scrap to recyclers rather than feeding it back.
Hot Runner vs Cold Runner: Side-by-Side Comparison
The table below compares the two systems across the dimensions that matter most in procurement decisions:
| Dimension | Hot Runner System | Cold Runner System |
|---|---|---|
| Initial cost | 30–50% higher mold price | Lower mold purchase price |
| Cycle time | Shorter; no runner cooling time | Longer; runners must solidify |
| Material waste | < 1% runner scrap | 15–25% runner scrap by weight |
| Maintenance complexity | Requires trained technicians; heater and thermocouple service | Tool-room staff can perform most repairs |
| Suitable production volume | > 5 million units/year | < 3 million units/year |
| Part quality | Tighter weight consistency; minimal regrind | Adequate; regrind must be managed |
When to Choose a Hot Runner PET Preform Mold
A hot runner system is the appropriate choice when:
- Annual volume exceeds 5 million preforms. The savings in material and cycle time accumulate quickly at scale. A 16-cavity mold running 24/7 can recover the higher initial investment within 12–18 months, depending on local PET resin prices.
- Part weight consistency is critical. Because each cavity is fed directly by a heated nozzle, variations from shear history and cooling differences are reduced. This matters for pharmaceutical and carbonated-beverage preforms that must meet tight gram-weight tolerances.
- Regrind must be minimized. Some brand owners limit post-consumer or post-industrial regrind content. A hot runner mold reduces scrap generation at the source.
- Fast color changes are needed. Valve-gate hot runner systems can purge faster than cold runner molds because there is no large solidified runner to remove between batches.
When to Choose a Cold Runner PET Preform Mold
A cold runner system remains the practical option when:
- Capital budget is constrained. The mold purchase price can be 30–50% lower than an equivalent heated-manifold system, which matters for startups or pilot lines.
- Production volumes are moderate. For annual needs below 3 million units, the payback period for the heated-manifold premium often extends beyond the typical mold life.
- Wide preform variety is required. Cold runner molds are easier to modify for different weights and neck finishes because the runner plate can be re-machined at lower cost than reconfiguring a heated manifold.
- Simpler maintenance is preferred. Local tool-room staff can usually handle traditional-runner repairs. Diagnostics for heated manifolds require specialized knowledge and spare parts that may not be immediately available in every region.
Cost Analysis: 3-Year Total Cost of Ownership
To illustrate how the two systems compare over time, consider a 16-cavity PET preform mold producing 28-gram water-bottle preforms at a nominal cycle of 12 seconds.
- Year 1: The heated-manifold mold carries a higher purchase price, but material savings begin immediately. The traditional-runner layout has lower upfront cost but generates runner scrap equal to roughly 20% of shot weight.
- Year 2: Assuming 6,000 production hours per year, the heated system avoids grinding, conveying, and drying the equivalent of several tons of runner material. Labor for runner separation is also eliminated. Energy costs are slightly higher for the heated system due to heater power, but the net operating cost still trends lower.
- Year 3: By the end of year three, the cumulative material savings of the heated system usually offset the initial price gap. The exact crossover point depends on local electricity rates, resin prices, and downtime patterns.
Processors should model these variables with their actual production schedule rather than relying on generic payback calculators.
Frequently Asked Questions About Runner Configurations
How long does a hot runner manifold last before overhaul? With correct temperature control and scheduled maintenance—thermocouple calibration, heater resistance checks, and nozzle cleaning—a heated manifold typically operates for 40,000 to 60,000 production hours before seals and heaters need a full overhaul. The manifold block itself often lasts as long as the mold frame.
Can an existing cold runner mold be converted to a hot runner layout? Conversion is possible but rarely economical. The A and B plates must be machined for a manifold cavity, cooling circuits relocated, and heater control wiring added. The combined machining and component cost usually reaches 70–85% of a new hot runner mold. If you need the features of a heated system, a new mold with the runner configuration designed in from the start is the lower-risk path.
Does preform quality differ between the two systems? For the preform itself, dimensional quality can be identical when both molds are designed and maintained correctly. The practical differences appear in weight consistency (valve-gate hot runners give tighter shot-to-shot weight control) and in contamination risk (cold runner regrind can introduce moisture and IV loss if drying is not managed). In PET applications, these differences matter most for long, thin-wall preforms used in carbonated beverages and hot-fill containers.
HEYAN’s Approach to Runner System Design
HEYAN (heyanmold.com) designs both heated-manifold and traditional-runner PET preform molds. The company was established in 2018; its core engineering team has worked in PET mold and machine engineering since the early 2010s. As of 2026, HEYAN holds 27 patents covering cavity layout optimization, valve-gate sequencing, and cooling channel geometry.
When a customer submits a Request for Quotation, HEYAN’s engineering team evaluates:
- Target annual production volume and shift pattern
- Preform weight, neck finish, and dimensional tolerance requirements
- Local resin supply and regrind policy
- Available plant utilities (chiller capacity, compressed air, power supply stability)
Based on this data, HEYAN recommends a runner configuration and provides a projected 3-year cost model. If a traditional-runner mold is selected, the runner layout is optimized to minimize pressure drop and achieve balanced filling. If a heated-manifold mold is chosen, HEYAN integrates nozzles and manifolds from established suppliers and designs the temperature-control architecture in-house.
Conclusion
Choosing between a hot runner and a cold runner PET preform mold is not about ranking one technology above the other. It is a matter of matching system characteristics to production realities. Heated-manifold molds reduce material waste and cycle time but demand higher capital outlay and specialized maintenance. Traditional-runner molds offer lower entry cost and simpler serviceability but generate runner scrap that must be managed.
For buyers evaluating a new line or mold replacement, the most reliable next step is to request a side-by-side quotation with a 3-year total-cost projection tailored to your specific preform specifications and operating hours.
Ready to compare runner systems for your next PET preform mold project? Contact HEYAN’s sales engineering team at [email protected] with your target part data, annual volume, and plant conditions. The team will return a runner-system recommendation and detailed cost projection within two business days.
Article prepared by the HEYAN 运营团队.