Description
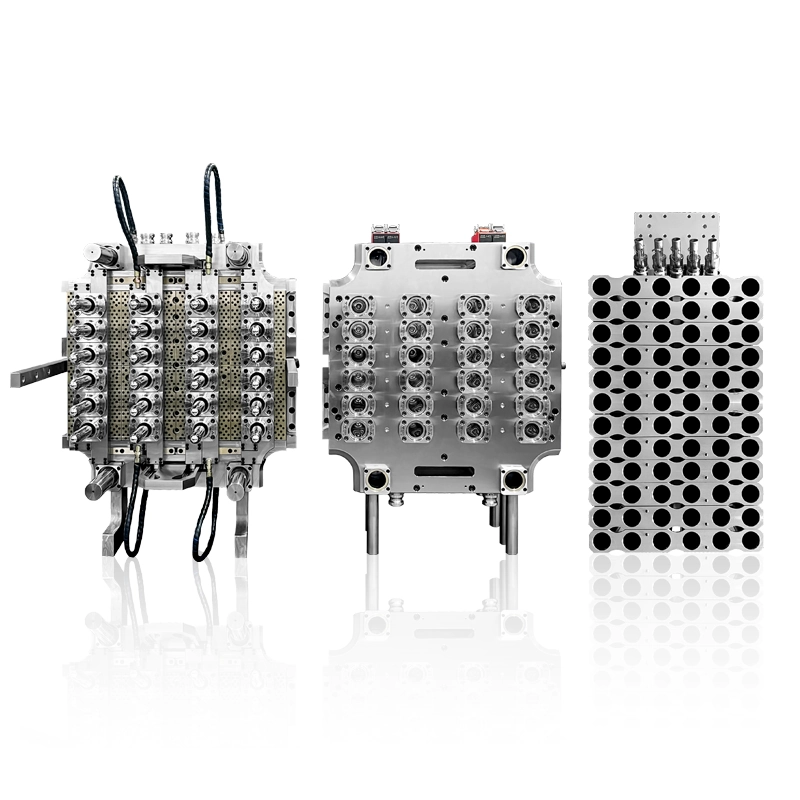
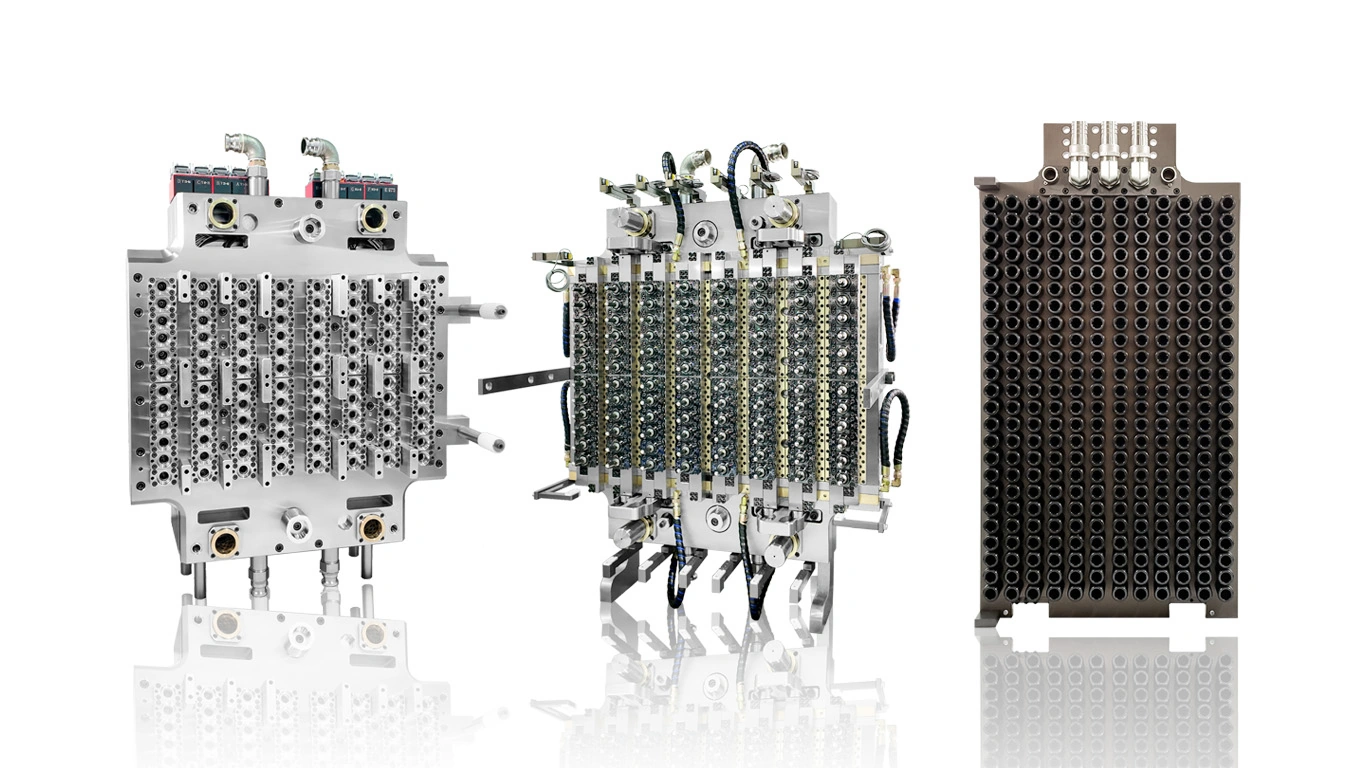
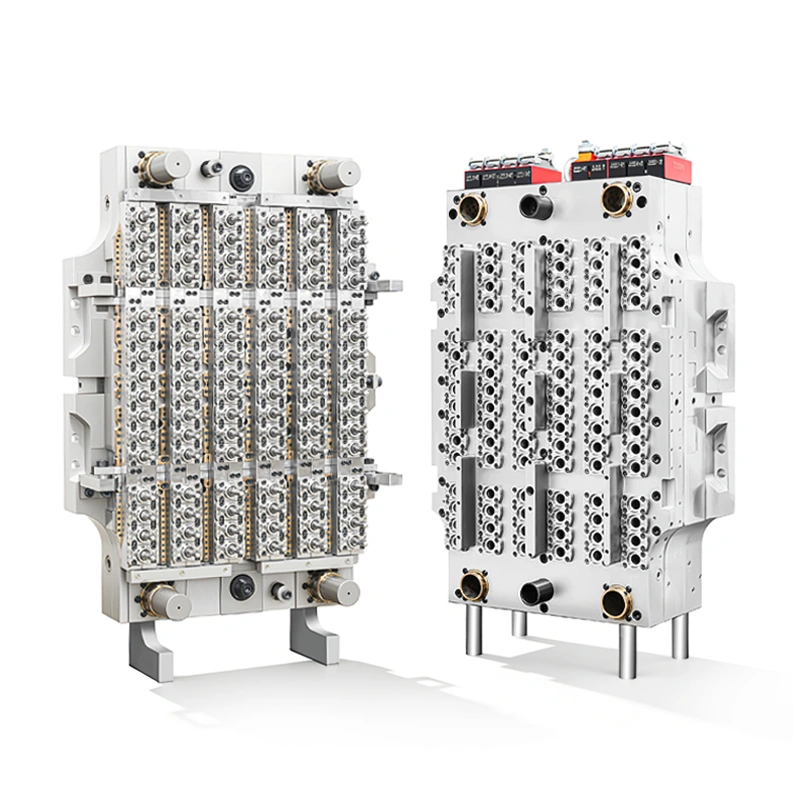
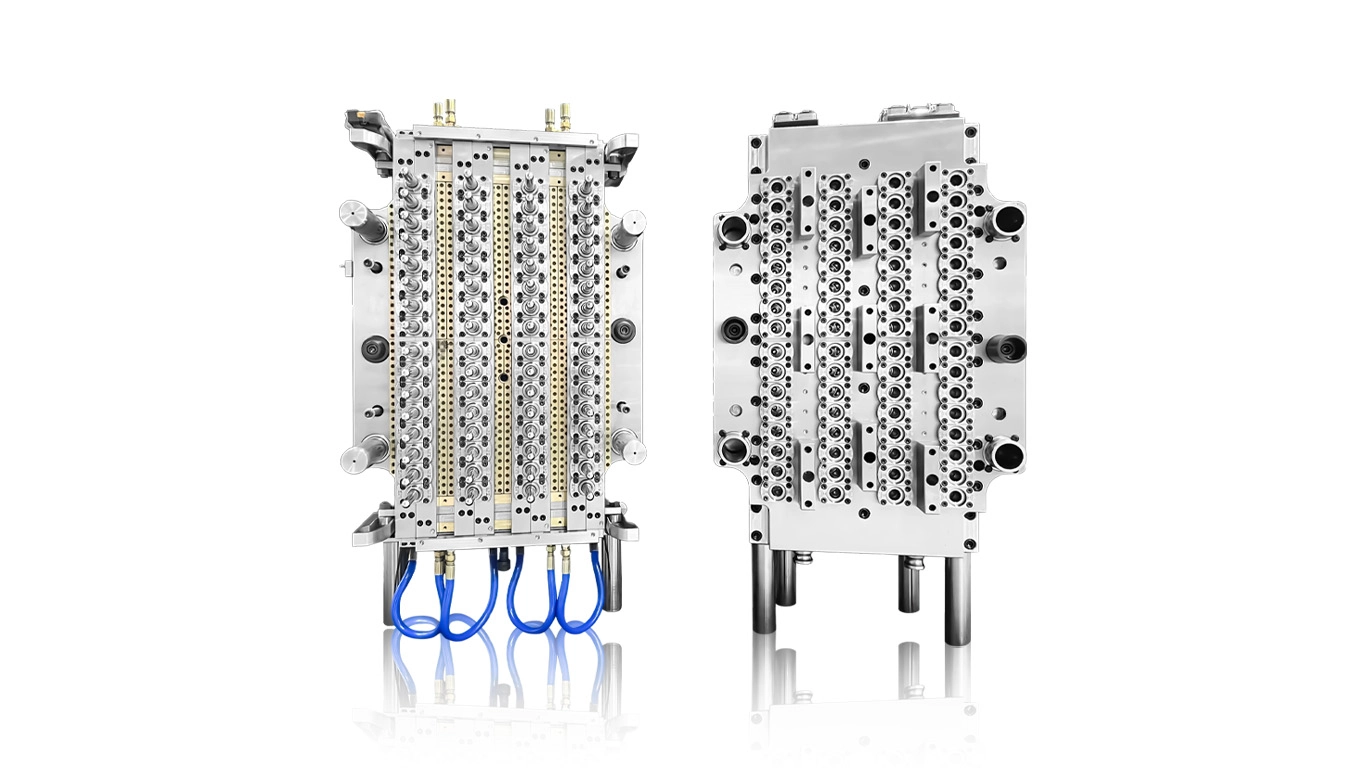
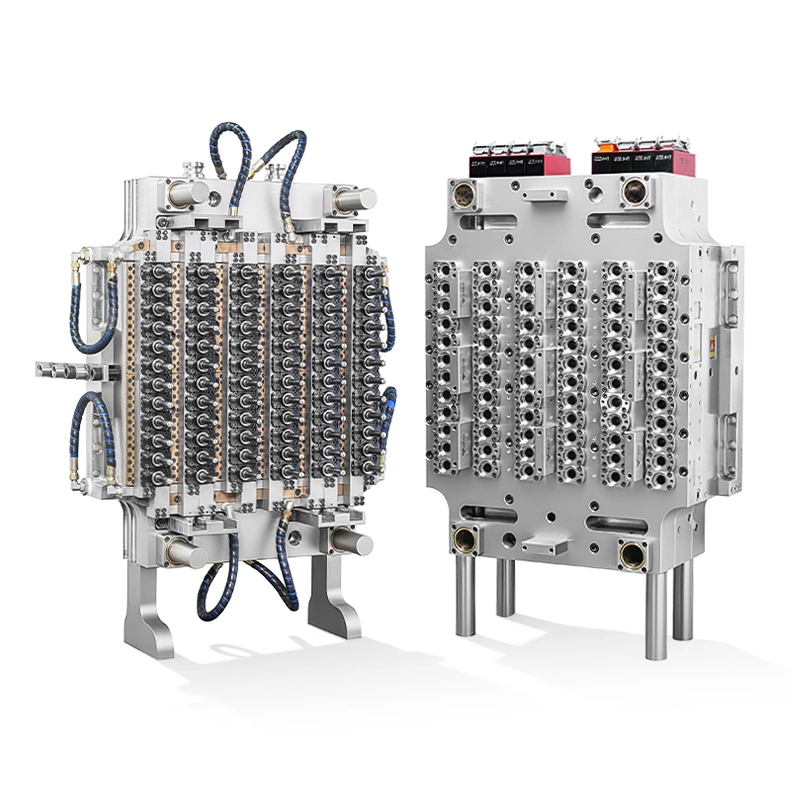

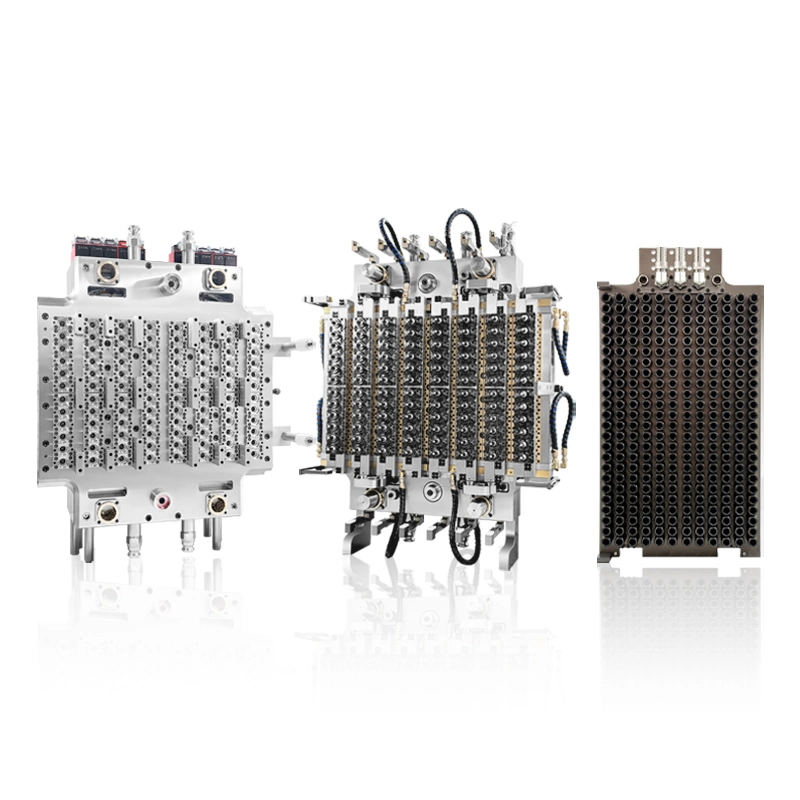
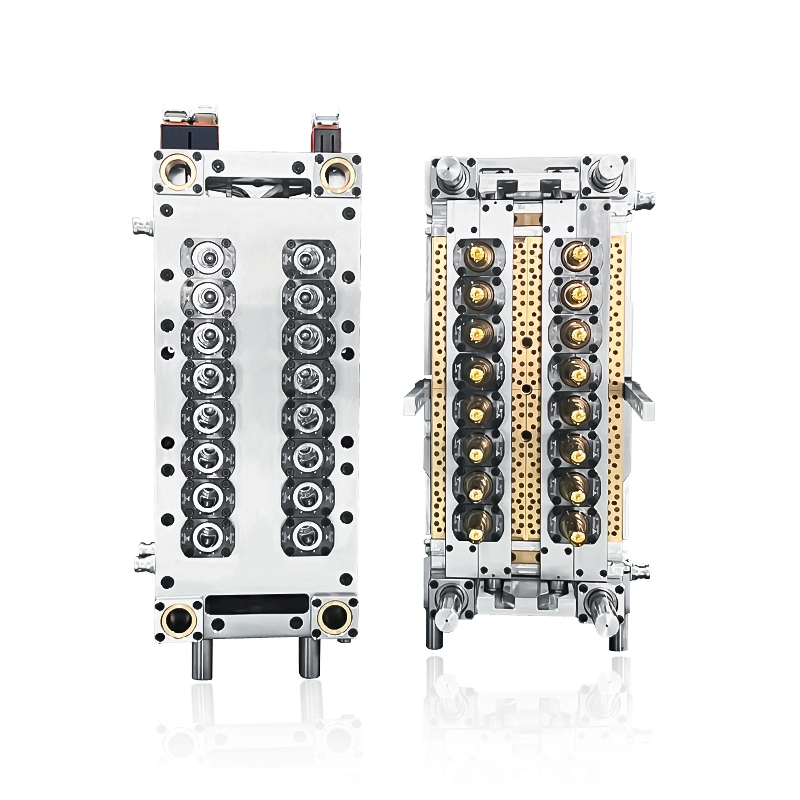
PET preform molds from 1 to 144 cavities with neck finishes including 3025, 2925, 1881, 1810, 38mm, 44mm, 55mm, oil bottle, and wide-mouth. Weight variation within ±3% of design value. Send your bottle drawing, target output, and factory layout for a compatibility-checked proposal.
Description
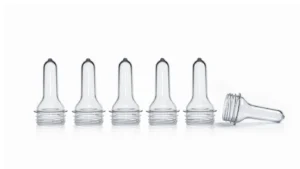
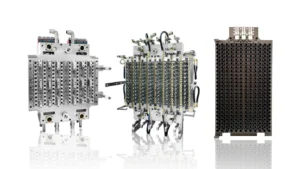
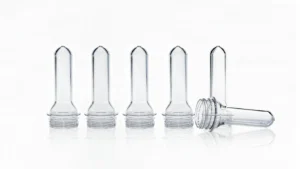
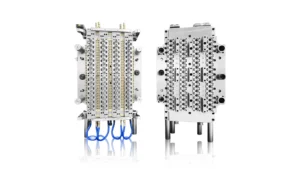
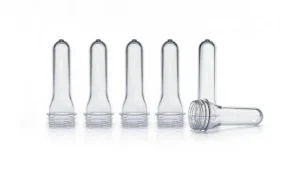
Product Overview
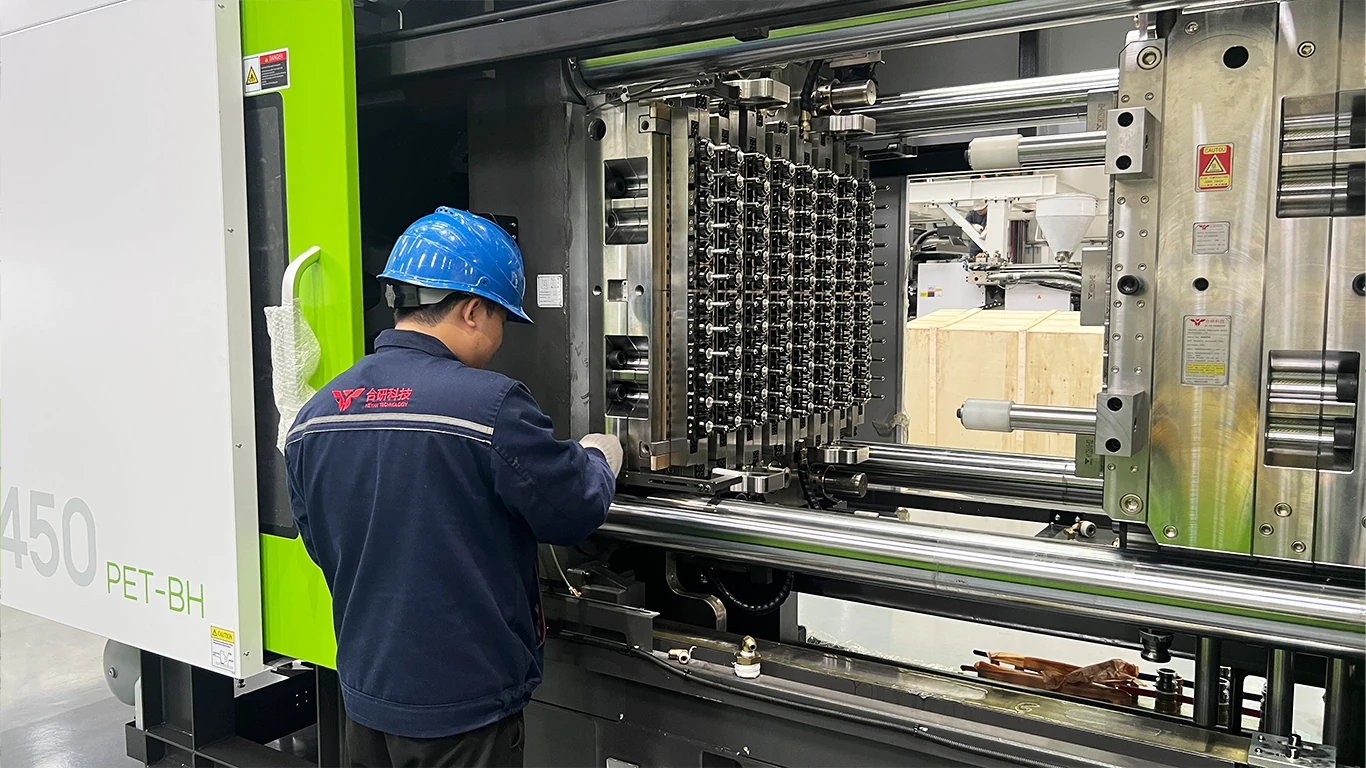
PET preform molds from HEYAN cover 1 to 144 cavities, with neck finishes including 3025, 2925, 1881, 1810, 38mm, 44mm, 55mm, oil bottle, and wide-mouth.
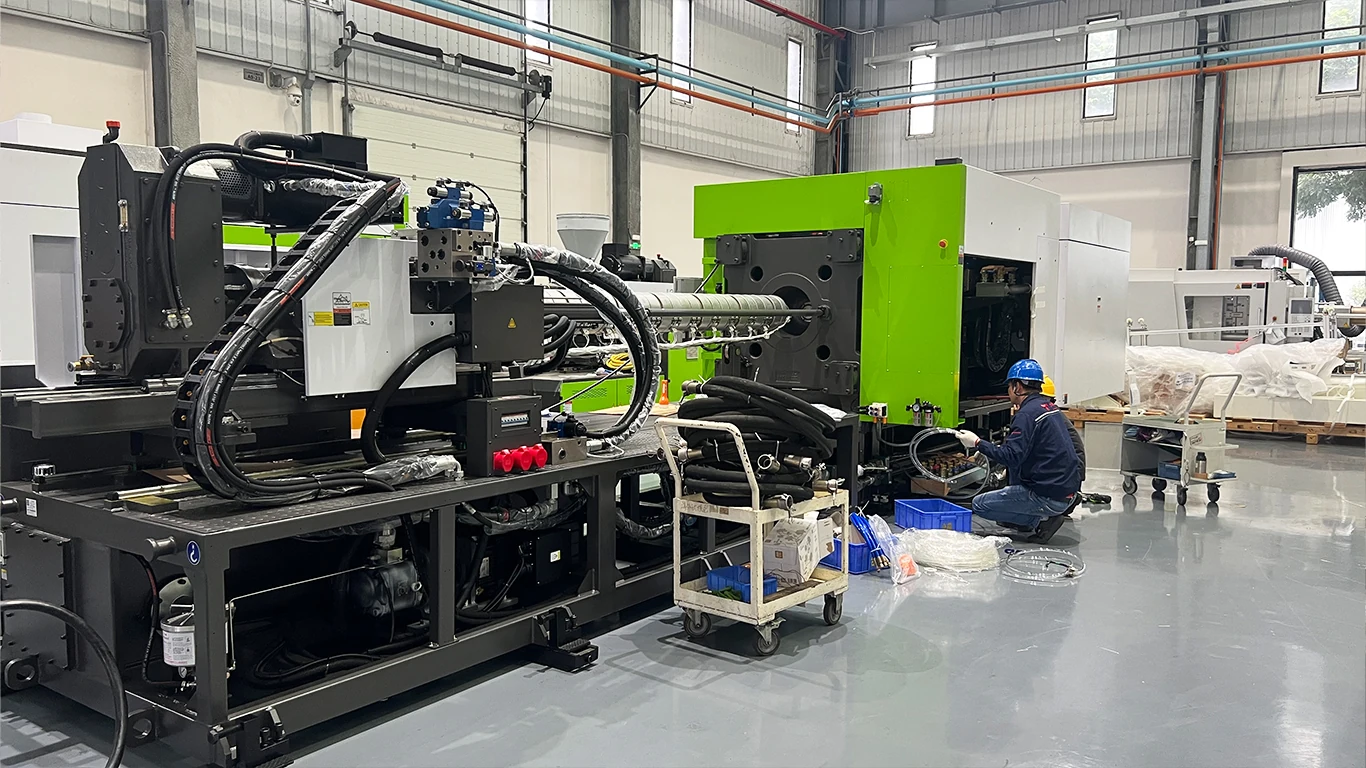
Weight variation stays within ±3% of the design value. Wall thickness, thread integrity, and seal surface quality are held to tolerances that match the blow molding process requirements. These parameters affect bottle strength, clarity, and production scrap rate. We do not sell molds as standalone components; instead, we verify compatibility across bottle design, preform geometry, neck finish, target output, PET injection machine, hot runner system, cooling layout, robot integration, and your factory utilities before quoting.
Technical Specifications
| Parameter | HEYAN Capability / Configuration Direction | Usage Boundary |
|---|---|---|
| Cavity Range | 1–144 cavities | Must be confirmed against injection machine clamp force, shot volume, preform weight, and target output |
| Application Volume | Approx. 50 ml–2,000 ml preform applications | Actual preform weight, neck finish, bottle design, and blow molding process must be confirmed |
| Core/Cavity/Neck Ring Material | S136LN (recorded product capability) | Specific project material and heat treatment subject to technical confirmation |
| Mold Base Material | 4Cr13 (recorded product capability) | Not all orders use the same configuration |
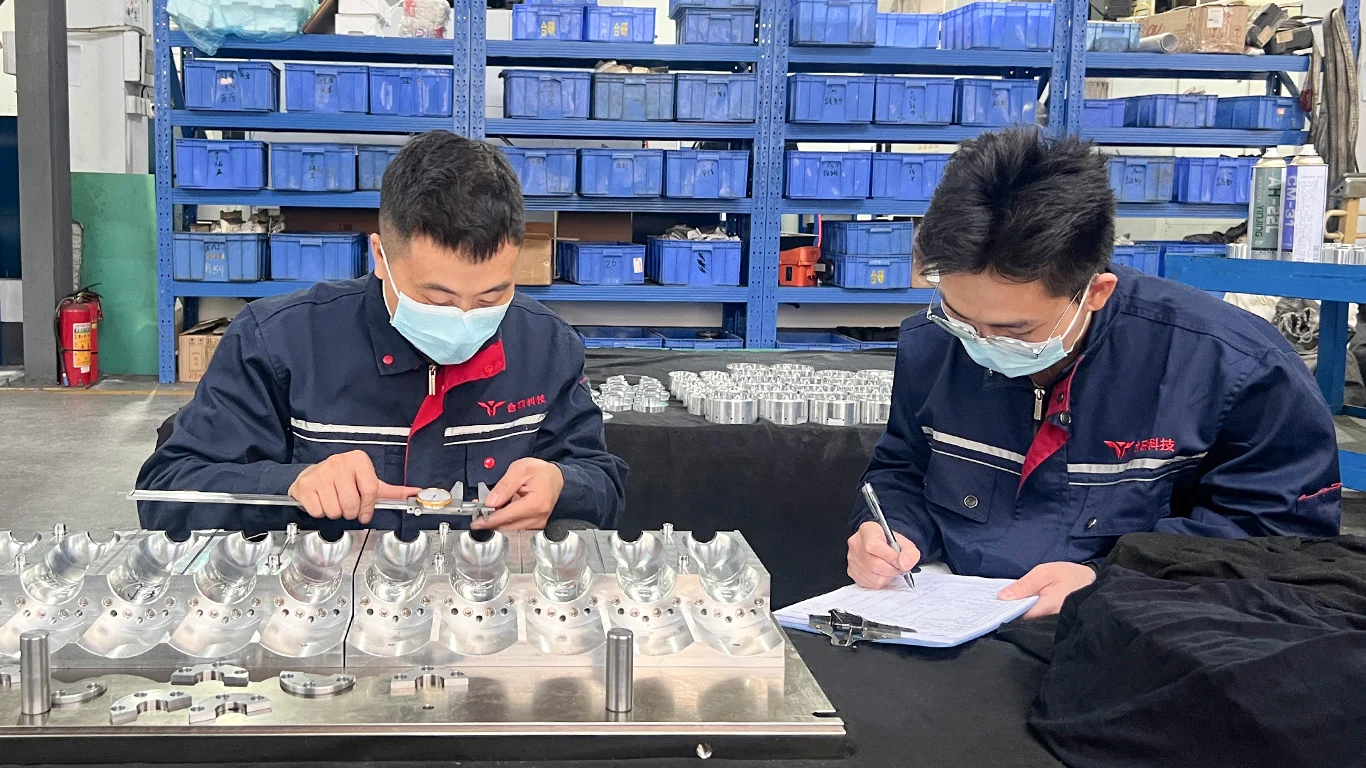
| Machining Precision | ±0.01 mm | Only used where corresponding components, datum, and inspection conditions are explicitly defined |
| Inspection Method | CMM (Coordinate Measuring Machine) | Inspection items, sampling ratio, and report format confirmed per project |
| Hot Runner & Cooling | Project-configurable PET hot runner and independent cooling circuits | Brand, structure, cycle time, and circuit count confirmed per proposal |
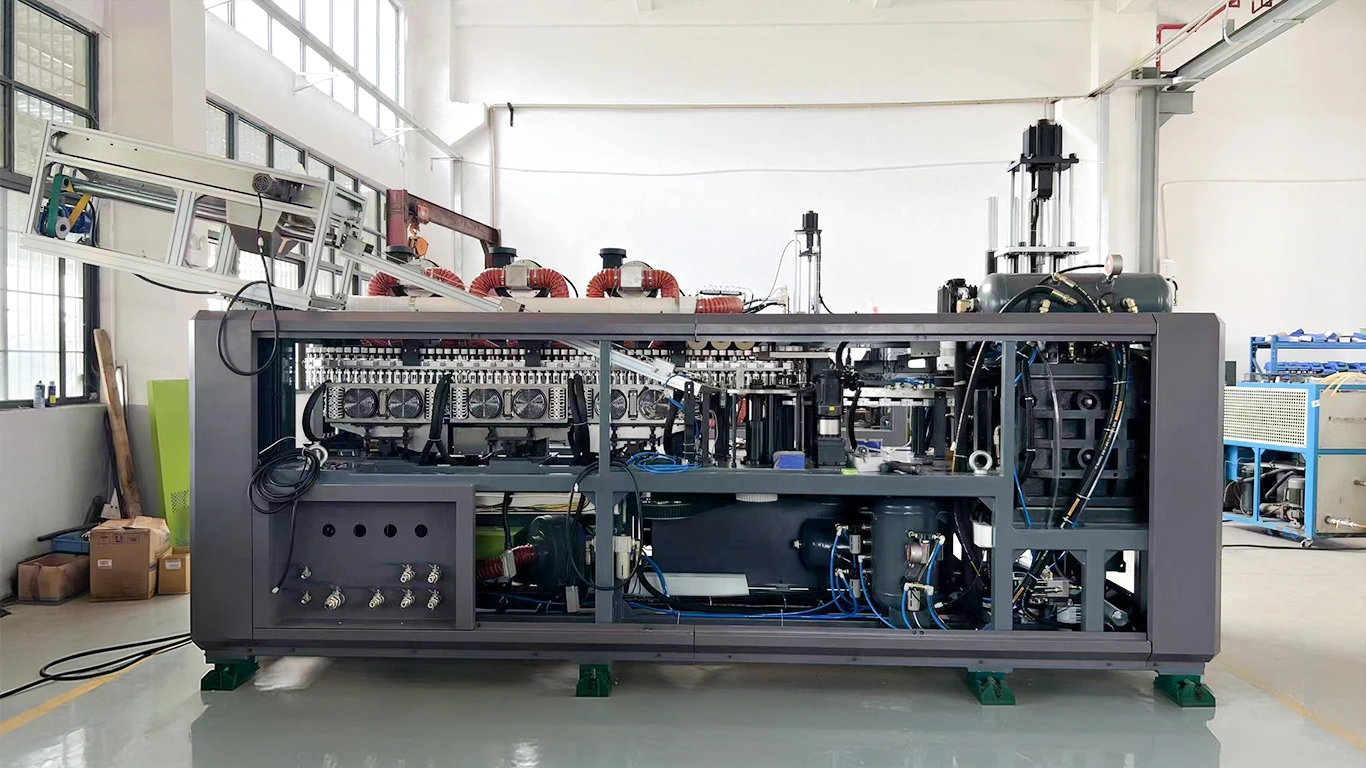
| Matching Capability | Compatible with PET injection machines, robots, drying, chillers, and material handling | Requires existing equipment or new line target parameters |
Injection Cycle Reference (Standard Machines)
Cycle times vary by neck finish and preform weight. Below are reference ranges for standard PET injection machines:
3025 Neck Finish
| Preform Weight | Injection Cycle | Cooling Time |
|—|—|—|
| 12g–14g | ~12–15 sec | 5–6 sec/cavity |
| 15g–17g | ~15–18 sec | 6–8 sec |
| 18g–21g | ~17–22 sec | 7–9 sec |
| 22g–25g | ~20–23 sec | 8–9 sec |
| 26g–30g | ~23–27 sec | 9–10 sec |
Note: Add 1–2 seconds for standard (non-high-speed) machines.
2925 Neck Finish
| Preform Weight | Injection Cycle | Cooling Time |
|—|—|—|
| 8g–10g | ~12 sec | 3–5 sec |
| 11g–13g | ~12–14 sec | 4–5 sec |
| 14g–16g | ~14–17 sec | 5–6 sec |
| 17g–20g | ~17–21 sec | 6–8 sec |
| 21g–23g | ~20–23 sec | 7–9 sec |
| 25g–27g | ~22–24 sec | 8–10 sec |
| 28g–30g | ~23–25 sec | 8–10 sec |
38mm Neck Finish
| Preform Weight | Injection Cycle | Cooling Time |
|—|—|—|
| 13g–15g | ~14–16 sec | 6–8 sec |
| 16g–18g | ~17–20 sec | 7–9 sec |
| 19g–21g | ~18–22 sec | 8–10 sec |
| 22g–25g | ~23–28 sec | 9–10 sec |
| 26g–30g | ~25–30 sec | 9–11 sec |
Additional neck finishes (1881/1810, 44/55mm, oil bottle, wide-mouth) available upon request with detailed cycle charts.
Standard Mold Base Dimensions
| Cavities | A (mm) | B (mm) | C (mm) | Weight (kg) | Matching Machine |
|---|---|---|---|---|---|
| 16 | 326 | 366 | 417 | 520 | 130T–160T |
| 24 | 366 | 406 | 457 | 680 | 160T–200T |
| 32 | 406 | 446 | 497 | 850 | 200T–260T |
| 48 | 466 | 516 | 567 | 1,200 | 260T–320T |
| 64 | 516 | 576 | 627 | 1,650 | 320T–400T |
| 72 | 546 | 606 | 657 | 1,900 | 400T–470T |
| 96 | 606 | 676 | 727 | 2,600 | 470T–550T |
What You Get
- Preform design support (bottle-to-preform mapping)
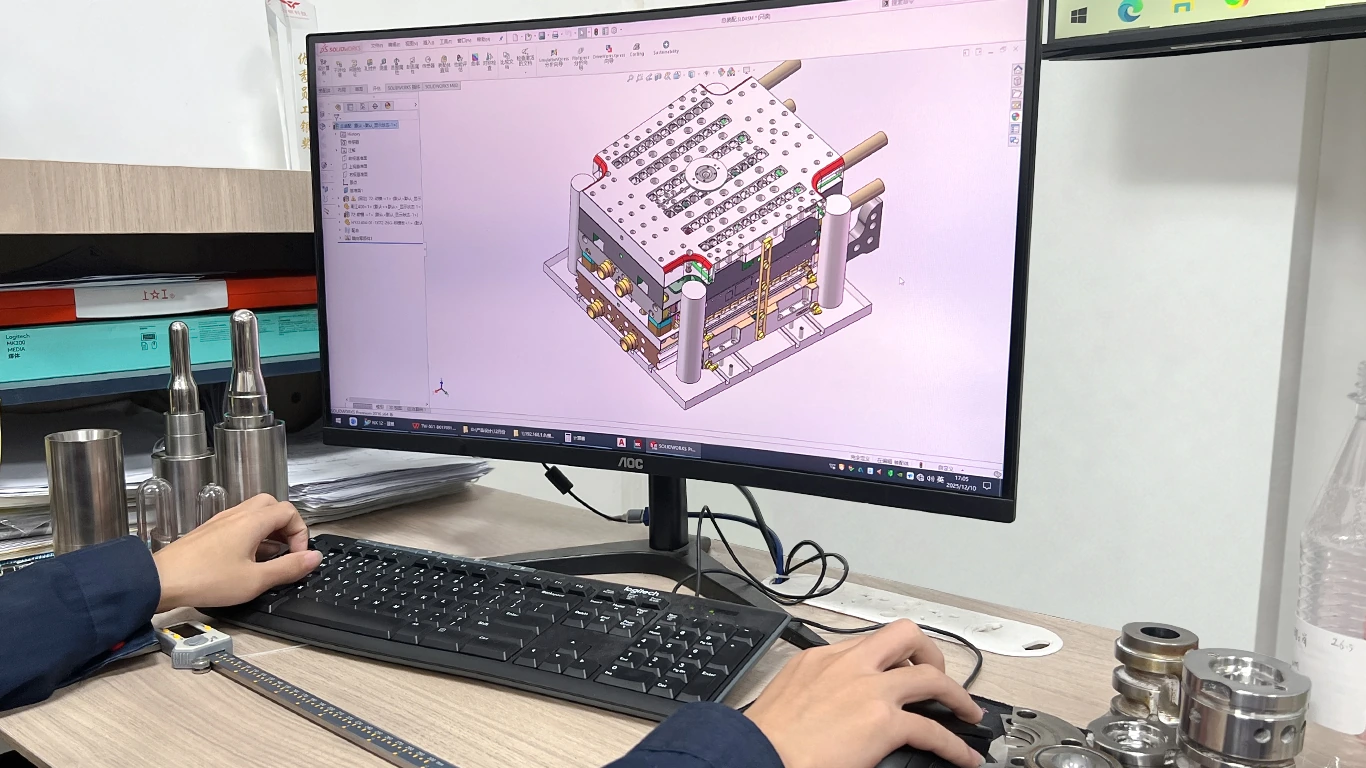
- Mold development with DFM review
- Trial samples and inspection reports
- On-site or remote installation and commissioning
- Operator training and start-up support
- Spare parts list and maintenance guidance
⚠️ Important Notes
- Do not quote by cavity count alone , injection machine platen size, tie-bar spacing, clamp force, shot volume, and ejection method must be verified first.
- Do not select preform by bottle capacity alone , same capacity can require different weight, neck finish, and wall-thickness distribution.
- Hot runner brand, structure, cycle time, and energy consumption are project-specific and not fixed across all orders.
- Mold life depends on material, heat treatment, production parameters, water quality, maintenance, and operation , subject to contract technical clauses.
- If the customer changes neck finish, preform weight, resin, or blow molding process, a re-evaluation is required.
Delivery
- Standard cavities (2–72): 45–50 days
- High-cavity (96): 50–55 days
- Express delivery available for selected configurations , contact us to confirm.
FAQ
Q1. What cavity range do HEYAN preform molds cover?
From 1 to 144 cavities, with neck finishes including 3025, 2925, 1881, 1810, 38mm, 44mm, 55mm, oil bottle, and wide-mouth. Weight variation stays within ±3% of the design value.
Q2. What information do I need to provide for a quote?
Bottle design, preform geometry, neck finish, target output, PET injection machine, hot runner system, cooling layout, robot integration, and factory utilities. We verify compatibility across all of these before quoting.
Q3. What materials and precision standards are used?
Core/cavity/neck ring in S136LN, mold base in 4Cr13, machining precision ±0.01 mm, with CMM inspection. Hot runner and cooling circuits are project-configurable.
Q4. Do you sell molds as standalone components?
We usually confirm the full production context (injection machine, cooling, robot integration, plant utilities) before quoting, to avoid mismatched configurations. Contact us with your line details for a tailored proposal.
Q5. What is the typical delivery time?
Delivery is confirmed per project after the design and compatibility review; reference mold delivery windows are listed in the Distribution section of our proposal.
Selection Guide
Three steps to a confirmed configuration:
- Define target output and preform weight — this decides cavity count and cycle target.
- Confirm neck finish (3025, 2925, 1881, 1810, 38/44/55mm, oil bottle, wide-mouth) and bottle design.
- Share your injection machine and plant utilities; we match hot runner, cooling circuits, and robot integration.
Ready to discuss your project? Send your bottle drawing, target output, and factory layout. We will confirm compatibility and return a detailed proposal.