When you start looking for a PET preform mold, one of the first practical questions is how many cavities you actually need. The answer comes down to three things: your daily output target, your bottle specs, and whether your injection machine can handle the mold.
Target Daily Output
Start from your production target and work backward. For standard neck finishes like PCO1810 or PCO1881, injection cycles usually fall between 12 and 28 seconds. Wide-mouth or heavy preforms run longer — large oil-container preforms in the 105g to 300g range typically need 40 to 75 seconds per cycle. Small-batch or trial work is better served by 8 or 16 cavities, which keeps tooling investment lower and gives you flexibility to switch bottle designs without replacing the whole mold.
Output is not a fixed number. It depends on cycle time, resin grade, cooling efficiency, and how well the mold is maintained. Treat any quoted figures as reference ranges, not guarantees.
Bottle Weight and Complexity
Heavier preforms or complex neck finishes need more cooling time per cycle, which pulls down effective hourly output. Thick walls or heavy weight mean fewer cavities and a longer cycle. Standard water bottles can use standard cavity counts. Wide-mouth or cosmetic bottles may need a specialized hot runner and a longer cycle.
Machine Compatibility
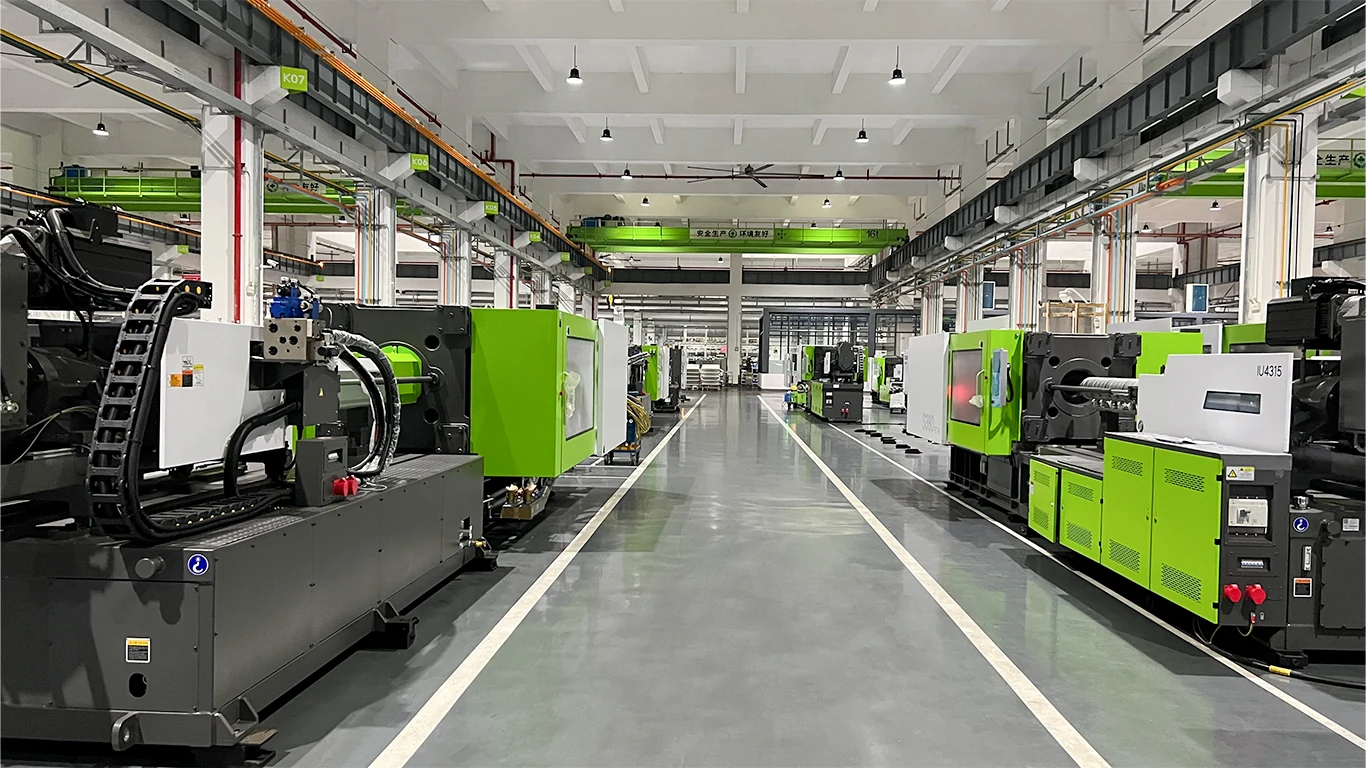
The mold has to fit your injection machine physically. Two practical checks: tonnage class and shot weight capacity. HEYAN standard mold bases start at roughly 16 cavities for 150-ton machine class and go up to 96 cavities for 500-ton class. Mold weights range from about 800kg to 3,100kg. Our PET injection machines cover shot weights from 800g to 6,000g. Before you commit to a cavity count, send your machine model or platen dimensions so we can confirm compatibility.
Configuration Reference
| Cavity Count | Typical Application | Machine Class Reference |
|---|---|---|
| 8–16 cavities | Startup, trial production, specialty bottles | Approx. 150-ton class |
| 24–32 cavities | Medium-volume water and beverage | Approx. 250–320-ton class |
| 48–64 cavities | High-volume bottled water | Approx. 320–350-ton class |
| 72–96 cavities | Large-scale production | Approx. 400–500-ton class |
Configuration, cycle time, and mold weight all shift with bottle design and machine setup. Send a bottle sample for an accurate assessment.
Get a Tailored Recommendation
HEYAN reviews your bottle sample, target output, machine specifications, and cooling setup before recommending a mold configuration. The goal is to balance production speed, consistency, and tooling life without pushing your equipment past its limits.
Send your bottle sample or 2D/3D drawing for a configuration recommendation within 2 business days.